 Jędrzej Siewierski
Author: Jędrzej Siewierski, CEO and co-founder of JSON Crew.
About 1,600 people enter the term „OEE” into Google per month (Google Ads data for Poland). Almost everyone gets the same pattern. The pattern is simple. The problem is that the result calculated from the paper is almost always too high.
The easiest way to see this is with the example of a bakery (this is an illustrative example, the numbers are conventional). The oven can bake one hundred loaves per hour. At the end of the shift, there are about two-thirds of what he could give on the shelves. The baker remembers that the oven once stood for forty minutes, and he remembers switching from bread to croissants. He can't remember twenty times when the dough stuck to the tape. He also didn't notice that the oven had been baking a little slower for a week because someone had set it up more carefully.
It measures this gap between what the machine could do and what it actually did well OEE. Below you can count them yourself and check why the card inflates the result.
In short:
- OEE answers three questions: whether the machine was working, whether it was working at full speed and whether it was making good pieces. Formula: availability × performance × quality.
- The losses are multiplying. The three results after 90% add up to only about 73%.
- OEE from manual reports is usually overstated and late: the card does not see short stops or slowdowns, and the weekly report comes when the problem has been going on for a long time.
Definition. OEE (from English Overall Equipment Effectiveness (OEE); (OEE);, in Polish, total equipment efficiency) is an indicator that tells what part of the planned machine operating time turned into good works done at full speed. OEE = Availability × Performance × Quality. 100% means that the machine produced only good pieces at the highest speed for the entire planned duration.
What is OEE? Three questions asked of the stove
A shift in a bakery lasts 8 hours, or 480 minutes. At best, the oven bakes 100 loaves per hour. If everything went perfectly, there would be 800 good loaves after the change. To understand where the rest has gone, we ask the stove three questions. Each has its own name in OEE.
Question 1: did the stove bake at all? It stood for 90 minutes (heater failure, switching from bread to croissants, waiting for the dough). So it only baked for 390 out of 480 minutes. This is availability: 390 / 480 = 81%.
Question 2: Was it baking at full speed? When he worked, he baked 85 loaves an hour instead of 100. The door opened every now and then, the belt stopped for a moment, more careful positioning. This is efficiency: 85 / 100 = 85%.
Question 3: Were the loaves good? Do sprzedaży nadawało się 95% upieczonych bochenków. The rest was burnt or crushed. This is quality: 95%.
We multiply: 81% × 85% × 95% = approximately 66%. Of the 480 minutes of a shift, only about 315 are really good work. The rest disappeared in three different places and each requires a different repair. This is the usefulness of OEE: the indicator shows whether the baker should look for lost time in stops, in pace or in misses.
How to calculate OEE? Formula and calculator
For a machine in your plant, the OEE formula looks like this:
| Hi | Pattern | What does he say? |
|---|---|---|
| Availability | (planned time − stops) / planned time | what part of the planned time the machine worked |
| Efficiency | (ideal cycle × number of total pieces) / working time | whether she was working at the speed she could afford |
| Quality | good arts/all arts | what part of the production is suitable for sending without corrections |
| OEE | availability × performance × quality | how much of the planned time is good production at full pace |
Illustrative example: 480 minutes of planned work, 60 minutes of stops, ideal cycle 30 seconds per piece, 700 pieces, of which 665 are good. Availability: 420 / 480 = 87.5%. Efficiency: 700 pieces of half a minute each is 350 minutes of work at an ideal pace. The machine worked for 420 minutes, so the efficiency is 83%. Quality: 665 / 700 = 95%. OEE: about 69%.
The most common mistake is a wrong ideal cycle. If you enter the average cycle over the last month instead of the fastest the machine can handle, the performance will come out to be close to 100% and the slowdowns will disappear from the bill. Take the cycle from the machine's documentation or the fastest repeatable one you have seen with your own eyes.
Try the calculator. First move the sliders for the bakery, then enter the numbers for your machine.
Set all three faders to 90%. The result is not 90%, but approximately 73%. Each loss takes away some of what the previous one left behind, so three „pretty good” results add up to an average one.
How much should OEE be?
OEE is associated with the name of the Japanese engineer Seiichi Nakajima and the TPM system (total maintenance, in which the operators also take care of the machines, and not only the maintenance department). According to English Wikipedia, the term OEE first appeared in his book TPM Tenkai from 1982.
The famous 85% is also associated with Nakajima. OEE.com writes that such a result is often considered world-class, and Nakajima treated it as the minimum worth striving for. Most manufacturing companies, however, have an OEE closer to the 60%.
Wikipedia notes, however, that calling the 85% world-class is in many cases a mistake. A machine for short series with frequent changeovers will never achieve the results of a line that produces one product all year round. What is more important than comparisons is whether your result increases and whether it is true.
Six great losses: where the machine's time flies
The losses are divided into six groups, called the six great losses (Wikipedia attributes this division to Nakajima's book Development Program from 1989). Each group goes into one of three parts of the pattern:
- Availability (machine standing): breakdowns, changeovers and adjustments.
- Performance (machine works too slowly): short stops and slowdowns.
- Quality (the machine makes shortages): deficiencies during start-up and deficiencies during production.
Click on a loss on the map below to see what it is in the bakery and plant and whether the card sees it. Then reduce it by half.
Look at the „Can the card see this” field. In this example, short stops and slowdowns take a total of 70 minutes and usually do not appear on the manual report at all. This is where the inflated result comes from.
Why does OEE calculated on a piece of paper lie?
In many plants, OEE is calculated from sheets of paper or from a sheet completed at the end of the shift. The operator enters the stops, the manager copies them into the table once a week and sends a report. It looks reliable, but it has three drawbacks. The same defects can be seen in every process in the company, not only in production (I write about it in article about process management in the company).
The card does not see short stops
The baker won't record that the dough stuck to the tape for a minute and a half. Not out of ill will. He corrected them, the furnace continues to work, nothing to write home about. The same applies to slowing down: the piece of paper knows the hours of work, but not the pace. The error always goes in the same direction, i.e. the result is better than in reality. Wikipedia notes that manual stop records can be less accurate than sensor records, although it's easy to start with.
The weekly report comes after the fact
If the furnace started burning slower on Monday and that week's report hits your desk on Wednesday of the following week, nine days pass before anyone can react. Engineers have a separate name for the interval between an event and the moment you see its effect: dead time. The longer it is, the later you react and the more you lose along the way.
When OEE becomes a premium
If the shift bonus depends on the OEE on the sheet, short stops start to go to the „planned break” column and misses to „fixes later”. Wikipedia explicitly warns in its description of OEE that if the indicator is poorly implemented, people may have a reason to bend the numbers. This is not a question of crew honesty, but a known phenomenon: when a measure becomes a goal, it stops measuring well. I describe them in more detail in the article about Goodhart's law.
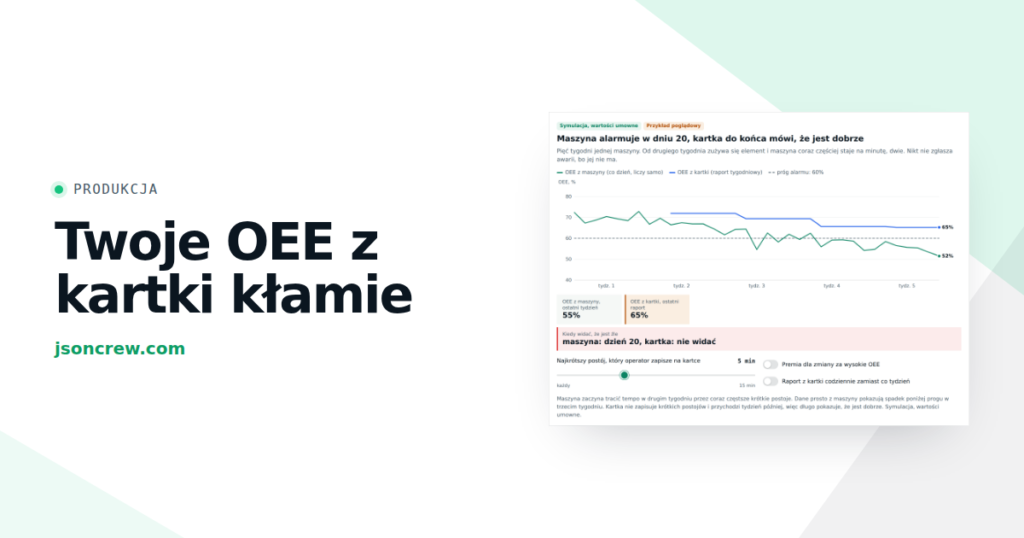
Below you can see all three flaws at once. This is five weeks of one machine, in which from the second week an element wears out, so it stops for a while more and more often. The green line is OEE calculated by the machine itself, the blue line is the report from the sheet. Move the stoppage record threshold and enable OEE bonus.
With default settings, the machine drops below the alarm threshold in the third week, and the chart shows over 60% by the end. The daily report reduces the delay, but still depends on someone recording every minute.
Live OEE: data straight from the machine
Imagine that the oven has a little counter that itself records every stop, every loaf baked and every loaf rejected. Nobody has to type anything. The meter sends data via the Internet to the panel where you see OEE from the last hour, not last week.
This is how IoT, or the Internet of Things, works: devices themselves send information about their work. In a plant, such a counter may be a machine controller, which often already knows the operating status and the number of cycles, or a simple module added to an older machine. When the data flows on its own, all three disadvantages of the paper disappear:
- You can see every stop. A stop of 40 seconds is recorded in the same way as a failure of 40 minutes. The slowdown is also visible because the machine knows its cycle.
- Latency drops from days to minutes. The slowdown is visible on the same day, not in the report next week.
- The result does not depend on who enters it. The bonus may stay, but no one is rewriting the numbers by hand.
With live data comes the next step. The first of the six great losses is failure, and failure rarely comes unannounced. First, there are more short stops, the pace drops, and the temperature increases. This can be seen on the green line in the simulation above. Predicting failures based on such signals is predictive maintenance. I write about him in article about predictive maintenance.
If you produce machines
Some readers of this text do not measure OEE, but produce and sell machines. If you are in this group, your customer still wants to know how much the machine really gives him. Show him this in the app from day one and you'll have a reason to contact him after the sale: inspection when there are short stops, parts before something breaks, upgrades when the machine becomes a bottleneck. On ours sales map this is the growth stage. We describe how we build applications for devices (mobile application, cloud and panel for the manufacturer) on the website IoT applications.
What to do on Monday
You don't have to start with sensors. Just four steps:
- Choose one machine, the one that is the bottleneck. That is, the one the rest of the plant is waiting for. Better OEE on a machine that is already waiting for others will not speed up overall production.
- Calculate OEE from the last week calculator above. Write down the result and its three parts.
- For one day, write down every stop, even a short one. Stand at the machine or ask the operator to do so, no bonus and no judgement. Compare the result with the paper. The difference is your invisible loss.
- Find out what the machine already knows. Many controllers know the operating status and the number of cycles. If the data is already there, reading it is usually easier than it seems.
When OEE won't help
- When the machine is not the bottleneck. Higher OEE on a machine that is waiting for material only gives you more inventory between stations.
- When orders are missing. OEE measures planned time. If the machine is standing there because there is nothing to do, it is a sales problem, not a production problem.
- When the result is used to punish. Then people correct the number, not the machine.
Where is your company blocking out?
OEE is just one area. In a company, the same three flaws (a measurement that misses some of the losses, a result that is a week late, and a number that has become a target) also appear in bidding, sales, service, and hiring. A short test will show where it is worst for you.
Where is your company blocking out?
Eight sentences about how your company responds to results. Next to each of them, indicate how often you do this. At the end, you will see what kind of regulator your company is today, what it lacks and where to start.
None of the eight sentences fit your business. This is a good sign: your decision loop is calm. Check it quarterly, because rocking usually begins when the company is growing or the market is changing.
I will send you 10 questions to list one process, with hints for your result
Sent
CEO of Ideo Solutions AS
Frequently Asked Questions
What is OEE in simple words?
OEE is the percentage of the machine's planned operating time in which it was making good pieces at full speed. It is calculated as the product of three indicators: availability (whether it worked), efficiency (whether it was at full speed) and quality (were the pieces good).
What is the formula for OEE?
OEE = Availability × Performance × Quality. Availability is working time divided by planned time. Efficiency is the ideal cycle multiplied by the number of all pieces and divided by the working time. Quality is good pieces divided by all pieces.
What OEE is good?
85% is often quoted as world level. OEE.com writes that Seiichi Nakajima treated such numbers as the minimum to strive for, and that most manufacturing companies have a result closer to 60%. What is more important than comparisons with other bets is whether your result is true and whether it is growing.
Why is OEE from manual reports inflated?
Because the card does not show short stops or slowdowns, and the weekly report arrives with a delay. When a bonus depends on the result, there is a temptation to include some stops as planned breaks.
Do I need a production management system (MES) or sensors to calculate OEE?
For starters, no. A piece of paper and a calculator are enough to know the order of magnitude and find the greatest loss. Data from the machine is needed when you want to see short stops, slowdowns and changes on an ongoing basis, not after a week.
OEE calculator
Do you want to check how much your machine really gives?
Return to the OEE calculator above, enter the data from the last change and compare the result with what is on the card. If the numbers are very different and you want to read data straight from the machine, write to us.
How to Cite This Article: Jędrzej Siewierski, „OEE: what is it, how to calculate it and why the result on the paper lies”, JSON Crew, jsoncrew.com, 2026.